Skip to content
A vertical baler vs horizontal baler comparison can become confusing when buyers focus only on price, pressure, or machine orientation. That approach can lead to waste accumulation, unsuitable bales, or unnecessary investment. I recommend comparing the machines against the material flow, required throughput, labor model, and downstream bale specifications.
The key difference between a vertical baler and a horizontal baler is how each machine fits the operating process. Vertical balers generally suit intermittent, lower-volume baling with more manual handling. Horizontal balers generally support higher-throughput or continuous workflows, with more feeding, tying, and discharge automation options.1 The correct choice depends on the material and required bale output.
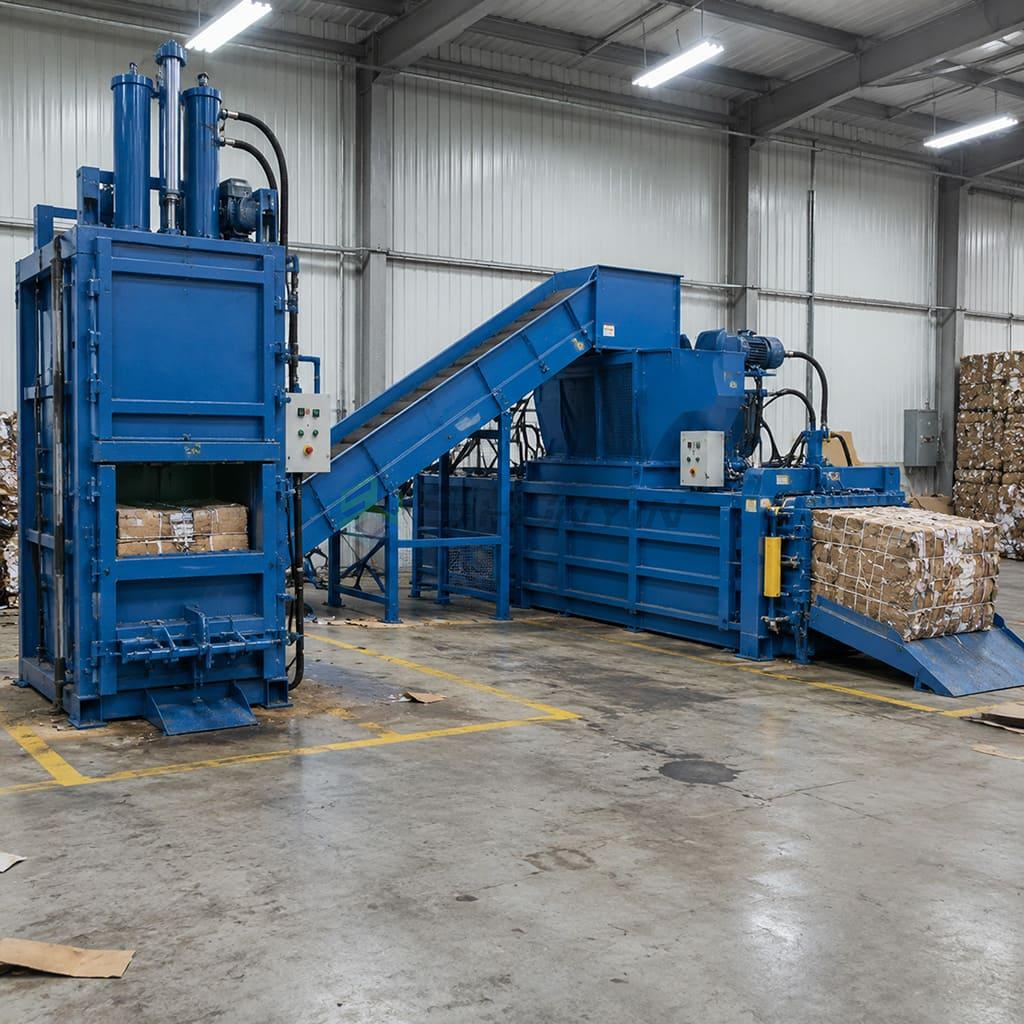
In my experience handling overseas baler inquiries, the best selection usually begins with questions rather than specifications. I first confirm what enters the machine, how quickly it arrives, how operators will handle it, and what bale must leave the facility. Those answers reveal which design deserves closer evaluation.
How Does a Vertical Baler vs Horizontal Baler Comparison Begin?
A buyer may request a machine quotation before defining the actual baling task. This creates a risk because two facilities processing the same broad material category can have very different operating needs. I start by examining the waste stream, operating schedule, available labor, storage process, and downstream bale requirements.
A vertical baler vs horizontal baler evaluation should begin with five points: material type, hourly or daily volume, feeding pattern, operating schedule, and required bale specifications. Buyers should also confirm labor availability, floor space, electrical supply, tying method, and downstream handling. Machine specifications become meaningful only after these operating conditions are documented.
I Start With the Material
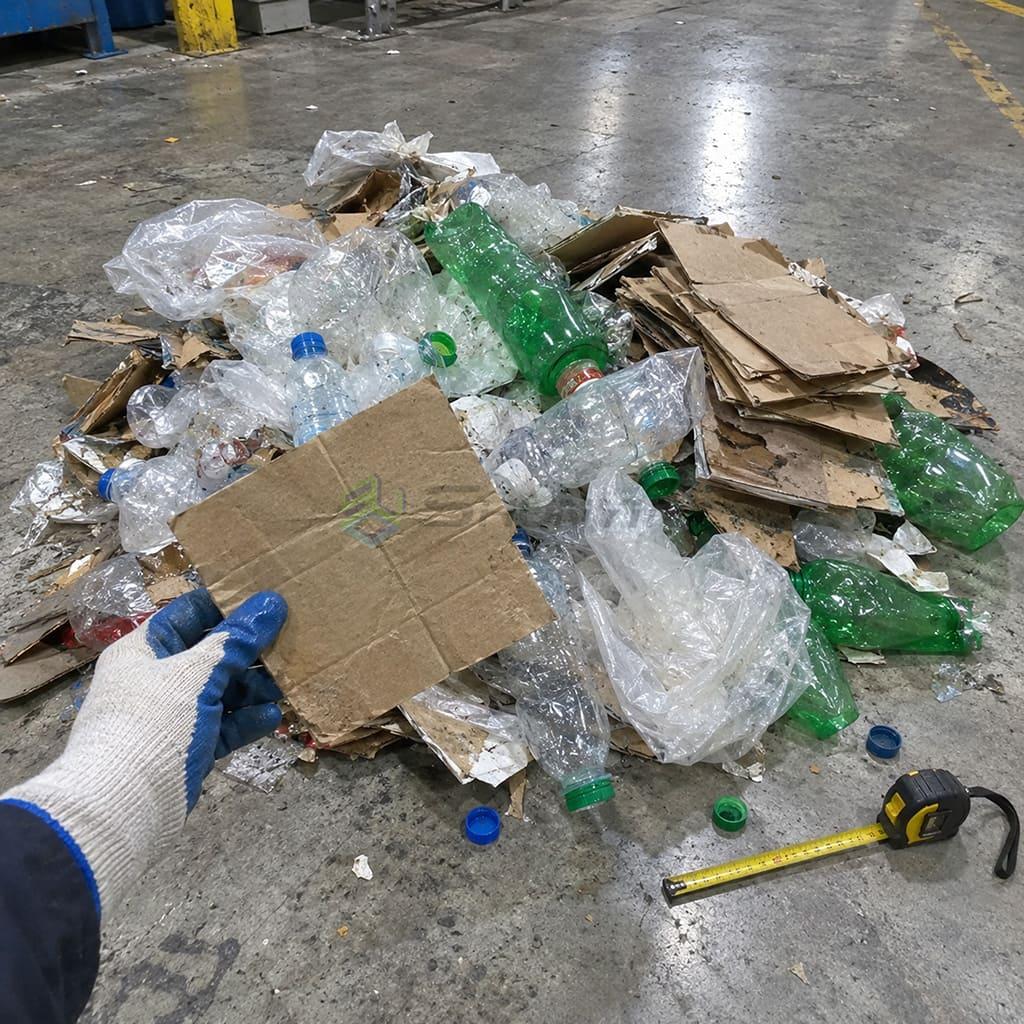
I do not treat cardboard, PET bottles, plastic film, textiles, and scrap metal as interchangeable materials. Each material behaves differently during feeding and compression.2
For example:
- Cardboard and OCC can vary in size, moisture, contamination, and whether boxes arrive flattened.
- PET bottles may include caps, residual liquid, labels, and different bottle shapes.
- Plastic film can be springy, slippery, or difficult to feed consistently.
- Textile waste can vary in fiber type, bulk density, and tendency to expand.
- Scrap metal requires equipment designed specifically for its strength and safety demands.
A model that performs well with one material may not produce the same throughput, density, or bale weight with another. I therefore ask buyers to send photographs, videos, material dimensions, estimated bulk density, and representative samples when practical. Material testing can be useful when the bale requirement is demanding or the material behavior is uncertain.
I Separate Daily Volume From Peak Flow
A daily tonnage figure does not tell the full story. I also ask how the material arrives.3
A facility may generate waste gradually during one shift. Another facility may receive several truckloads within two hours. Although their daily totals could be similar, the second operation needs enough feeding and processing capacity to avoid a backlog.
I usually document:
- Average volume per hour or shift
- Peak incoming volume
- Number of operating hours
- Number of working days
- Expected growth
- Current accumulation between baling cycles
- Time available for feeding, tying, and bale removal
The buyer should verify throughput against a defined material and test condition. A supplier’s headline capacity may represent favorable feeding, prepared material, or continuous operation. Actual output can change with operator behavior, conveyor performance, material moisture, and required bale density.4
I Define the Bale Before Selecting the Machine
I ask where the bale will go after it leaves the chamber. This question often changes the recommendation.
The downstream party may require:
- A particular bale cross-section
- A target weight range
- Stable dimensions for truck or container loading5
- Specific wire, strap, or tying arrangements
- Sufficient bale integrity for forklift handling
- A density range suitable for storage or resale
The phrase vertical baler vs horizontal baler describes two machine categories, but it does not confirm whether either proposed model can make the required bale. I recommend obtaining written bale specifications from the recycler, paper mill, plastics processor, shipping partner, or end user. The machine supplier can then assess those requirements against the material and configuration.
I treat advertised values as a starting point. I confirm critical output requirements through technical review and, when needed, a representative material test.
When Is a Vertical Baler Usually the Better Fit?
Some buyers assume that a vertical machine is automatically the cheapest or simplest choice. That assumption can overlook labor, material behavior, and bale requirements. I generally consider a vertical baler when the facility has intermittent material flow and can accommodate manual feeding, tying, and bale removal procedures.
A vertical baler generally fits lower-volume or intermittent waste streams where operators can load batches manually and complete tying cycles as required. It can suit warehouses, retail distribution sites, printing plants, and smaller recycling operations. However, its suitability still depends on material characteristics, required bale dimensions, target weight, safety controls, and verified model performance.
I Look for a Batch-Based Workflow
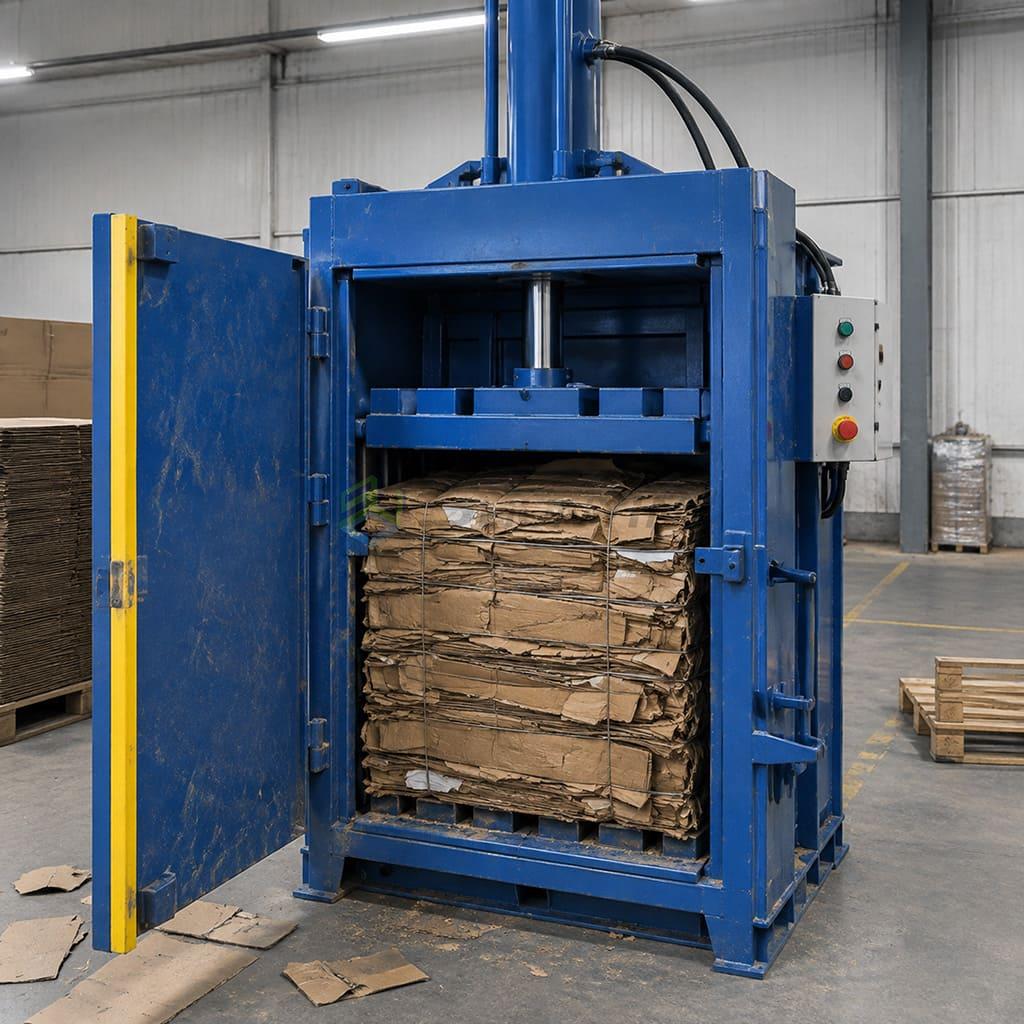
A vertical baler commonly works as a batch machine.6 An operator opens the loading door, places material into the chamber, starts the compression cycle, and adds more material until the bale is complete. The exact sequence depends on the model and control design.
This arrangement can be practical when:
- Waste accumulates gradually
- An operator can visit the machine at intervals
- Manual loading is acceptable
- Bale tying frequency is manageable
- The finished bale can be removed safely
- Very high continuous throughput is not required
- The available footprint favors a compact layout
Vertical designs can also help businesses move away from loose waste without immediately installing conveyors or a larger automated line. I have seen buyers benefit from this simpler approach when their incoming material volume did not justify a horizontal system.
I Account for Labor Beyond Loading
Buyers sometimes compare equipment prices but leave labor out of the calculation. I ask who will prepare the material, load the chamber, monitor cycles, tie the bale, remove it, and move it into storage.
Manual handling can include:
- Breaking down oversized cardboard
- Sorting contamination
- Loading repeated batches
- Positioning wire or strapping
- Tying the completed bale
- Opening the discharge system
- Removing and transporting the bale
- Cleaning around the machine
The total labor requirement depends on the machine configuration and local process. Buyers should observe or simulate a full bale cycle rather than considering only the hydraulic compression time.7
I Check Practical Limitations
A vertical baler is not automatically suitable because it occupies less floor area or has a lower quoted purchase price. I also check ceiling height, door swing, bale ejection space, forklift access, installation clearance, and the operator’s working area.
The following comparison shows the general questions I use. It does not replace model-specific verification.
| Evaluation point | Vertical baler tendency | What I verify |
|---|---|---|
| Material arrival | Often intermittent | Peak volume and accumulation risk |
| Feeding | Commonly manual | Material size and loading height |
| Tying | Often manually completed | Tie type, count, and cycle time |
| Bale removal | Batch discharge | Ejection method and safe clearance |
| Labor | Usually more operator involvement | Full-cycle labor requirement |
| Installation | Often simpler | Foundation, height, access, and power |
| Expansion | May be limited by batch workflow | Future material growth |
In a vertical baler vs horizontal baler decision, I do not reject the vertical option simply because the customer expects growth. Instead, I estimate future peak flow and determine whether the proposed model has reasonable operating margin. If the machine would need to run constantly just to keep up, a different design may deserve evaluation.
When Does a Horizontal Baler Better Support the Workflow?
A facility can lose efficiency when incoming waste exceeds a batch machine’s practical feeding rate. Loose material then occupies floor space and requires repeated handling. I consider a horizontal baler when the operation needs a steadier flow, larger production capacity, or integration with conveyors and other processing equipment.
A horizontal baler generally supports higher-throughput or more continuous operations. Depending on its configuration, it can accept conveyor feeding, provide automatic compression cycles, use automated or semi-automated tying, and discharge bales with less manual intervention.8 Buyers should choose it only when the material flow, bale requirements, labor savings, and projected utilization justify the added investment.
I Examine the Complete Feeding System
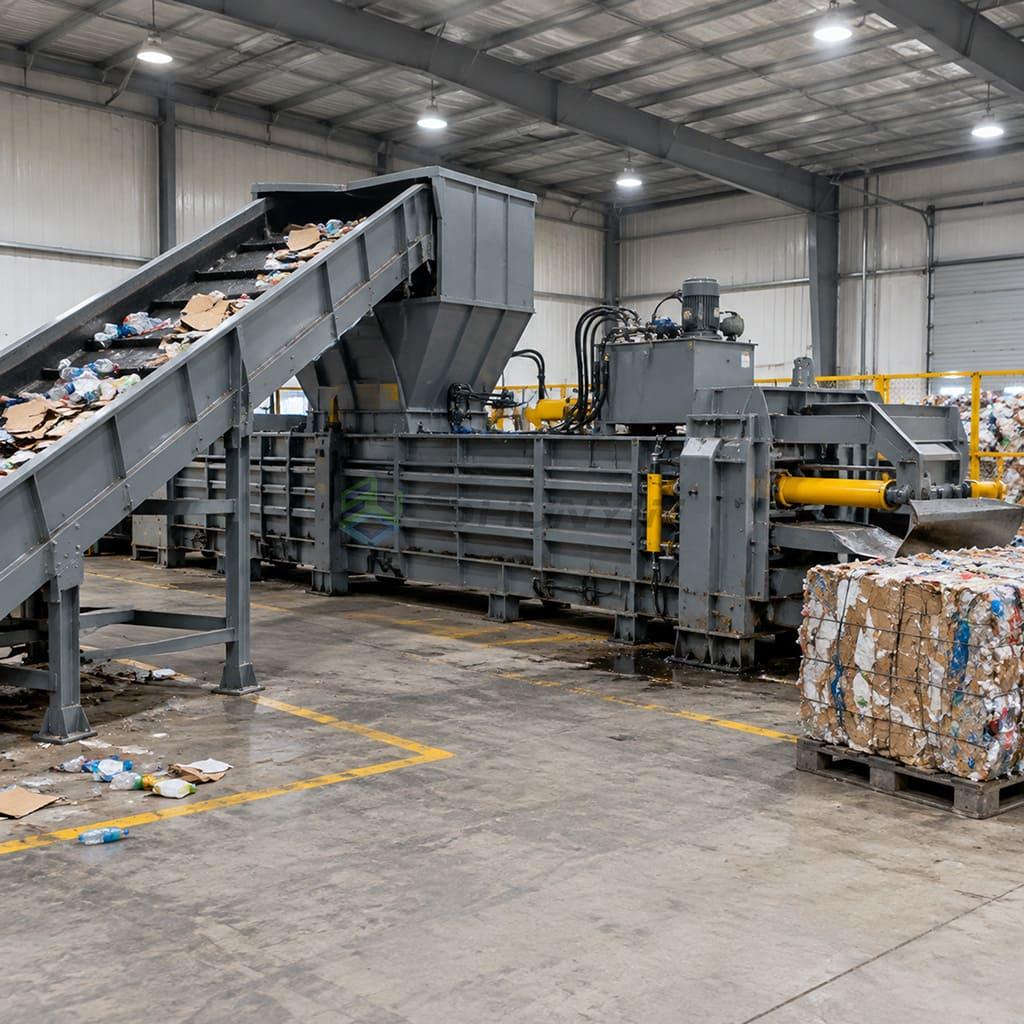
A horizontal baler does not operate in isolation. Its effective output depends on how material reaches the feed opening. A correctly sized baler can still underperform if the conveyor, loading equipment, or sorting line delivers material unevenly.9
Possible feeding methods include:
- Inclined belt conveyors
- Chain conveyors
- Forklift or loader feeding
- Air conveying systems for suitable materials
- Manual feeding stations
- Connections from sorting or shredding equipment
I evaluate the baler and feeding system together. The conveyor width, speed, incline, sidewall design, and control logic should match the material. Light film behaves differently from flattened OCC, and loose PET bottles can move differently from denser industrial scraps.
Sensors and interlocks also affect the workflow. Buyers should confirm how the feed conveyor communicates with the baler, what happens during overload conditions, and whether operators can access clearing points safely.
I Compare Automation by Function
The word “automatic” can mean different things in supplier quotations. I ask the supplier to identify each automatic and manual action.
| Function | Questions I ask |
|---|---|
| Feeding | Does a conveyor feed continuously or only on operator command? |
| Compression | Does the cycle start from a sensor, timer, or manual control? |
| Tying | Is tying manual, semi-automatic, or fully automatic? |
| Bale length | How is bale length measured and adjusted? |
| Discharge | Does the bale exit automatically, or does it require assistance? |
| Line control | Are conveyor and baler controls integrated? |
| Fault recovery | What actions must an operator perform after a jam or alarm? |
This functional review makes a vertical baler vs horizontal baler comparison more useful than a simple automation label. It also helps buyers estimate staffing needs and training requirements.
I Avoid Oversizing the Machine
Horizontal balers can provide higher throughput, but higher capacity has little value when a facility cannot feed the machine consistently. An oversized system may increase capital cost, electrical infrastructure, maintenance needs, and occupied space without creating a proportional benefit.10
I recommend estimating utilization under average and peak conditions. Buyers can consider:
- Current throughput
- Expected three-to-five-year growth
- Shift structure
- Seasonal variation
- Material availability
- Conveyor loading rate
- Downstream storage capacity
- Truck or container dispatch schedules
No universal capacity figure applies across every material and configuration. Published output should be tied to a verified model, feed method, material condition, and test basis.
I Review Installation and Support
A horizontal system may require more planning for shipping, unloading, positioning, foundation work, conveyor installation, electrical integration, and commissioning. I ask overseas buyers to review these requirements before placing an order.
I also recommend confirming:
- Installation drawings
- Machine and conveyor dimensions
- Foundation or anchoring requirements
- Connected electrical load
- Hydraulic oil specifications
- Wear and spare parts lists
- Remote and on-site support options
- Operator and maintenance documentation
- Warranty terms and exclusions
- Expected spare-parts dispatch process
Buyers should request applicable safety and conformity documents, but they should treat certifications as records to verify rather than as substitutes for technical evaluation.11 Local engineers, safety professionals, and authorities should review application-specific installation and compliance requirements.
How Do Bale Specifications Affect a Vertical Baler vs Horizontal Baler Decision?
Buyers sometimes select a baler by feed volume and then discover that the finished bale does not meet shipping or downstream acceptance requirements. This creates additional handling and may reduce transport efficiency. I therefore treat bale dimensions, weight, density, tying, and stability as primary selection criteria rather than secondary preferences.
Required bale output can determine whether a vertical or horizontal baler is suitable. Buyers should specify the material, target bale dimensions, acceptable weight range, tying method, density expectations, and handling process. The supplier must then confirm whether a particular model and configuration can achieve those results, preferably through documented testing when the requirement is critical.
I Learned This From a Saudi PET-Bottle Inquiry
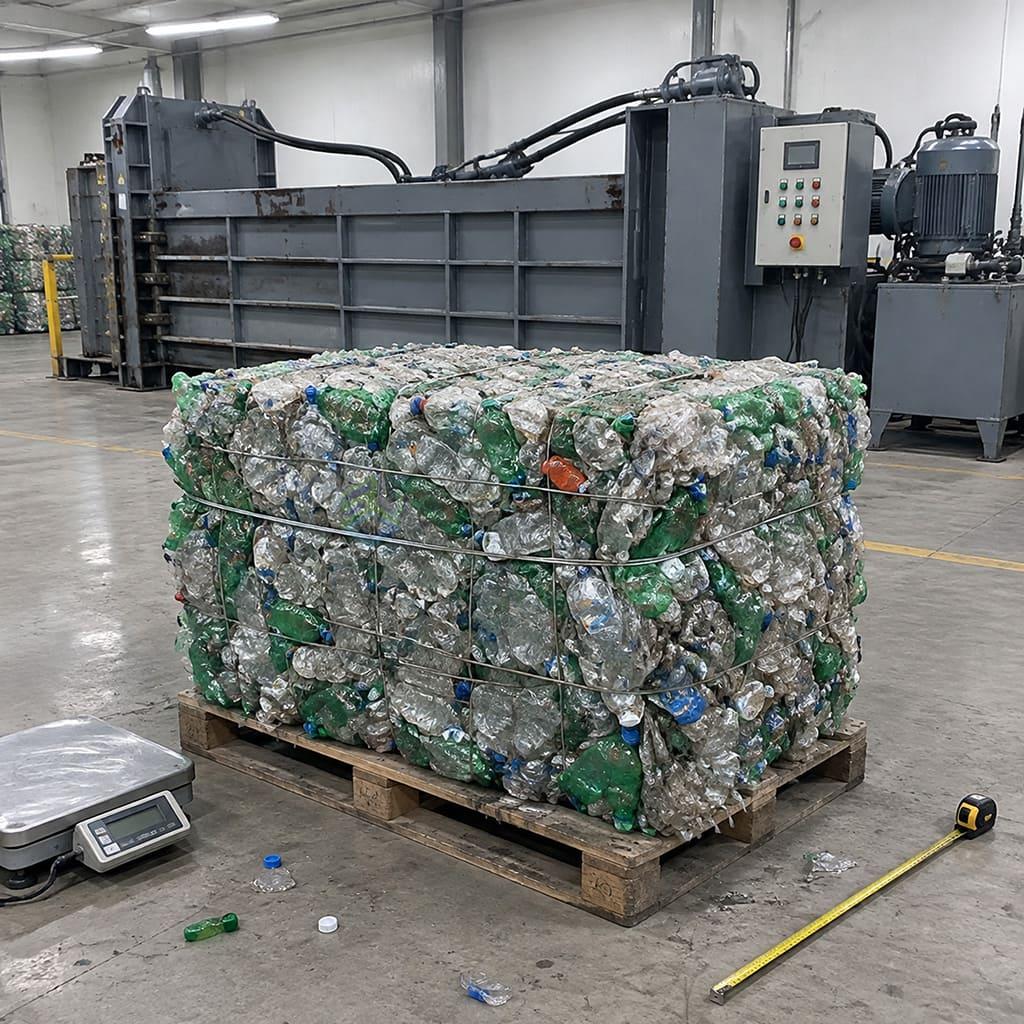
One inquiry from Saudi Arabia showed me why orientation alone does not decide the application. The customer wanted to process PET bottles and had defined requirements for bale size and weight.
The proposed vertical solution could not meet that requested combination. I did not want to offer a machine based only on a general statement that vertical balers can process PET bottles. The real question was whether that specific machine could produce the customer’s required PET bale.
I sourced PET bottles and arranged a material test. The purpose was not to claim a universal result for all PET streams. The test helped the customer see how the material behaved and why the required output called for a horizontal hydraulic baler in that specific application.
The customer purchased the horizontal baler and later reported satisfactory long-term use. I treat this as a bounded customer example, not as proof that every PET application needs a horizontal machine. Bottle preparation, residual liquid, perforation, caps, feed consistency, and target bale specifications can all change the result. Any unpublished measurements from that test would require verification before being used as performance claims.
I Distinguish Bale Weight From Compression Force
Compression force matters, but it does not independently determine bale weight or density.12 The result can also depend on:
- Chamber dimensions
- Material bulk density
- Material elasticity
- Feed preparation
- Number and sequence of compression cycles
- Retention or counter-pressure
- Bale length settings
- Tying method
- Moisture and contamination
- Operator technique
- Machine condition
This is why I avoid comparing machines by a single pressure figure. The stated force may also be presented in different units or calculated under different assumptions. Buyers should ask whether the value represents nominal, maximum, or normal operating force and how it relates to the proposed material.
I Request a Clear Test Protocol
When bale output is critical, I recommend defining the test before it begins. A useful protocol can record:
- The material type and source
- The condition of the material
- Any sorting, flattening, shredding, or perforation
- The machine model and configuration
- The feeding method
- Bale dimensions
- Bale weight
- Tie type and number
- Cycle conditions
- Any deviations or operator interventions
Qualified technical professionals should review safety-critical or application-specific conclusions. A supplier test can support preliminary machine selection, but it does not replace local risk assessment, installation engineering, or independent verification when a contract requires it.
How Should Buyers Compare Vertical and Horizontal Baler Suppliers?
A suitable machine design can still become a poor investment when the supplier does not confirm the application, document the configuration, or support the equipment after delivery. I encourage buyers to evaluate manufacturing quality, technical communication, testing capability, spare-parts planning, and service procedures alongside the quoted price.
Buyers should compare baler suppliers using a written application specification and a model-specific quotation. The review should cover materials, throughput assumptions, bale requirements, feeding and tying systems, component brands, safety controls, manufacturing inspections, testing, documentation, warranty, spare parts, installation, and after-sales support. Certifications should be requested and independently verified where relevant.
I Ask for a Model-Specific Technical Proposal
A useful quotation should identify more than the machine name and total price. I expect the proposal to state the selected configuration and the assumptions behind it.
My review normally covers:
- Machine model
- Intended material
- Recommended throughput basis
- Feed opening and chamber dimensions
- Proposed bale dimensions
- Expected bale output, with stated conditions
- Tying arrangement
- Conveyor or feeding equipment
- Electrical standard
- Hydraulic and control components
- Safety devices
- Included spare parts
- Installation responsibilities
- Delivery schedule
- Warranty and service terms
If a supplier promises a bale weight or hourly output, I ask for the material and operating conditions behind that statement. Broad ranges can mislead buyers when they are copied across different materials.
I Review Manufacturing Quality Controls
For either machine type, manufacturing quality can affect frame alignment, hydraulic reliability, cylinder life, control stability, and long-term maintainability. I encourage buyers to request inspection records appropriate to the order.
Relevant checkpoints can include:
- Incoming steel and component verification
- Welding procedure and welder qualification records
- Dimensional inspections
- Hydraulic pressure and leakage checks
- Electrical cabinet inspection
- Sensor and interlock testing
- No-load and material testing
- Surface preparation and coating inspection
- Final assembly checks
- Packing and loading documentation
The exact checks should match the machine and contract. Buyers should also decide whether they need a factory acceptance test, live video inspection, third-party inspection, or pre-shipment inspection.
I Calculate More Than Purchase Price
A vertical baler vs horizontal baler cost comparison should include the operating process, not just the equipment invoice.
I suggest reviewing:
| Cost area | Questions to evaluate |
|---|---|
| Labor | How many people handle feeding, tying, and removal? |
| Energy | What is the connected load and expected duty cycle? |
| Consumables | What wire, strap, oil, and wear parts are required? |
| Installation | Are conveyors, foundations, wiring, or lifting needed? |
| Maintenance | Which components need routine replacement? |
| Downtime | How quickly can technical help and parts arrive? |
| Logistics | Will the bale dimensions improve storage and shipping? |
| Utilization | Will enough material be available to use the capacity? |
The lower-priced machine can become expensive if it creates a bottleneck. However, the more automated machine can also waste capital if incoming volume remains too low. I use total process fit as the deciding principle.
Frequently Asked Questions
Is a horizontal baler always better than a vertical baler?
No. I generally recommend horizontal balers for higher or steadier throughput, but they are not universally better. A vertical baler may be more practical for intermittent waste, limited production volumes, and operations that can manage manual loading and tying. The final choice requires model-specific and material-specific evaluation.
Can both baler types process cardboard and PET bottles?
Many models can process these materials, but capability varies by chamber design, feeding method, compression system, and bale requirement. I do not assume that one model can process every cardboard or PET stream. I recommend confirming material condition, throughput, target bale size, bale weight, and tying requirements with the supplier.
Which baler requires less labor?
A horizontal baler with conveyor feeding and automatic tying can reduce manual handling, depending on its configuration. However, operators may still need to sort material, monitor feeding, clear faults, and move finished bales. I compare the complete workflow rather than relying on the word “automatic.”
How can I verify a supplier’s stated baler capacity?
I ask the supplier to define the tested material, feed condition, operating time, machine configuration, and measurement method. I also request test videos or a witnessed material trial when output is critical. Buyers should place verified performance conditions in the purchase specification or contract.
What information should I send before requesting a quotation?
I recommend sending material photographs or videos, daily and peak hourly volume, operating hours, required bale dimensions and weight, available power supply, labor expectations, floor-space limits, feeding preference, and destination country. Representative material samples can support testing when performance requirements are difficult to confirm remotely.
Conclusion
A vertical baler vs horizontal baler decision should begin with the task rather than the machine. I evaluate the material, peak throughput, feeding pattern, labor model, operating schedule, and required bale output before recommending a design. Vertical balers often fit intermittent, lower-volume workflows, while horizontal balers often support continuous feeding and greater automation. Neither option is automatically superior.
If you are comparing balers for an overseas recycling project, send us your material details, capacity needs, and required bale specifications. Our team can review them and prepare a preliminary, model-specific equipment recommendation for further professional evaluation.
"[PDF] City of Gustavus Capital Improvement Plan", https://gustavus-ak.gov/2393/Capital-Improvement-Plan-2026-2030. Waste-management guidance generally characterizes vertical balers as batch-oriented machines with substantial operator involvement and horizontal balers as systems more readily integrated with continuous feeding and automated tying or discharge; these are typical configurations rather than universal limits for every model. Evidence role: definition; source type: institution. Supports: Independent waste-management guidance should describe vertical balers as commonly batch-loaded and manually tied and horizontal balers as more readily integrated into continuous or automated material-handling systems.. Scope note: The distinction is categorical and contextual because individual models may depart from the usual configuration. ↩
"Effect of raw material properties and die geometry on the density of ...", https://bioresources.cnr.ncsu.edu/resources/effect-of-raw-material-properties-and-die-geometry-on-the-density-of-biomass-pellets-from-composted-municipal-solid-waste/. Experimental studies of waste compaction report that densification behavior depends on material composition, initial bulk density, particle or package geometry, moisture, elasticity, and friction, supporting material-specific evaluation rather than treating recyclable streams as mechanically interchangeable. Evidence role: mechanism; source type: paper. Supports: Research should show that compaction response and feeding behavior vary with material properties, including initial bulk density, geometry, elasticity, moisture, and friction.. Scope note: Laboratory compaction results may not directly predict the performance of a particular commercial baler. ↩
"[PDF] Rethinking Load Growth", https://nicholasinstitute.duke.edu/sites/default/files/publications/rethinking-load-growth.pdf. Capacity-planning and queueing theory show that average demand alone does not determine congestion: when arrivals vary or temporarily exceed service capacity, material queues and backlogs can develop even if total daily input appears manageable. Evidence role: mechanism; source type: education. Supports: Capacity-planning literature should establish that systems sized only to average demand can develop queues when arrivals are variable or temporarily exceed processing capacity.. Scope note: Queueing theory supports the general sizing principle but does not specify the required capacity of a particular baler. ↩
"Effect of roller layout on biomass bales quality and ... - BioResources", https://bioresources.cnr.ncsu.edu/resources/effect-of-roller-layout-on-biomass-bales-quality-and-baling-energy-consumption-during-rotary-compression/. Baling and compaction studies indicate that measured capacity is conditional on feed consistency, material moisture and preparation, equipment utilization, and the target density or compression cycle, so nominal output is not necessarily equivalent to sustained field throughput. Evidence role: mechanism; source type: paper. Supports: Empirical research should demonstrate that baling or compaction capacity is conditional on feed rate, material condition, operator or process continuity, and target density.. Scope note: Evidence from agricultural or biomass baling may establish the mechanism but may not directly quantify performance for recyclable-waste balers. ↩
"Protecting Perishable Foods During Transport by Truck or Rail", https://ask.ifas.ufl.edu/publication/HS1328. Unit-load and cargo-transport guidance identifies dimensional consistency as relevant to load planning, space utilization, stacking, and cargo securing during road or container transport. Evidence role: general_support; source type: institution. Supports: Transport or unit-load guidance should explain that consistent dimensions facilitate load planning, space utilization, securing, and safe handling.. Scope note: Such guidance establishes the logistical relevance of consistent dimensions but does not define the optimal dimensions for a specific recyclable material or shipping route. ↩
"Evaluation Of Solid Waste Baling and Balefills, Volume 1 and 2", https://nepis.epa.gov/Exe/ZyPURL.cgi?Dockey=2000TC07.TXT. Government machine-safety guidance describes common vertical-baler operation as a sequence of chamber loading, platen compression, additional loading as needed, manual or assisted tying, and discrete bale ejection, consistent with a batch workflow. Evidence role: definition; source type: government. Supports: Government safety or operating guidance should describe the usual vertical-baler sequence of chamber loading, compression, repeated loading, tying, and bale ejection.. Scope note: The described sequence is typical of downstroke vertical balers and may not cover every specialized configuration. ↩
"(PDF) Tutorial on Work Systems Cycle Time Analysis of Manual Work", https://www.academia.edu/22092911/Tutorial_on_Work_Systems_Cycle_Time_Analysis_of_Manual_Work. Work-measurement methodology defines total process time as the combined duration of manual tasks, machine operation, handling, and unavoidable delays; hydraulic compression time alone therefore does not represent the labor or duration of a complete bale-production cycle. Evidence role: mechanism; source type: education. Supports: Industrial-engineering sources should establish that total cycle time includes manual, machine, delay, and handling elements and therefore cannot be inferred from machine actuation time alone.. ↩
"[PDF] On September 24, 1996, a 17-year-old male laborer ... - CDC Stacks", https://stacks.cdc.gov/view/cdc/167416/cdc_167416_DS1.pdf. Technical descriptions of horizontal baling systems document configurations incorporating conveyor feeding, sensor-initiated compression cycles, automatic or semi-automatic tying, and continuous or assisted bale discharge, although the installed functions vary by machine design. Evidence role: general_support; source type: institution. Supports: Independent technical guidance should document the use of conveyors, automatic cycling, tying mechanisms, and continuous or assisted discharge in horizontal baling installations.. Scope note: The source would support the availability of these functions, not establish that every horizontal baler includes them. ↩
"(PDF) Improving Home Appliance Assembly Line Throughput Using ...", https://www.academia.edu/83252027/Improving_Home_Appliance_Assembly_Line_Throughput_Using_Discrete_Event_Simulation_and_Cellular_Manufacturing. Production-line research identifies upstream starvation and feed variability as causes of reduced downstream utilization and throughput, meaning that nominal machine capacity cannot be realized when conveyors or sorting stages deliver material inconsistently. Evidence role: mechanism; source type: paper. Supports: Production-systems research should show that downstream machines lose utilization when upstream stages cannot supply material at a sufficient and stable rate.. Scope note: The systems principle is directly relevant, but the magnitude of the loss must be measured for the particular baler line. ↩
"[PDF] UC Davis - OSTI", https://www.osti.gov/servlets/purl/3409798. Engineering and energy-management guidance notes that oversized equipment can impose higher acquisition, installation, electrical-capacity, maintenance, and space costs while spending more time at low utilization, where the additional rated capacity may provide little operational value. Evidence role: general_support; source type: government. Supports: Energy-management or engineering guidance should explain that oversized equipment can carry higher purchase, installation, energy-demand, maintenance, and space costs while operating at low utilization.. Scope note: General equipment-sizing guidance does not by itself establish the cost penalty for a specific baler installation. ↩
"SHIB 08-13-2013 - Operating Hazards of Baler Discharge-Door Locks", http://www.osha.gov/publications/shib081313. Machinery-safety authorities state that conformity documentation or marking does not eliminate the need for workplace-specific risk assessment, safe installation, guarding verification, operator training, and controls for foreseeable use and maintenance. Evidence role: expert_consensus; source type: government. Supports: Authoritative machinery-safety guidance should state that conformity marking or documentation does not remove the user’s duty to assess risks associated with installation, use, maintenance, and the specific workplace.. Scope note: The precise legal duties and required documents vary by jurisdiction and by whether the party is a manufacturer, importer, employer, or equipment user. ↩
"Effect of Compaction Pressure and Moisture Content on Post ...", https://pmc.ncbi.nlm.nih.gov/articles/PMC7917922/. Compaction research treats final bulk density as a function of applied pressure together with material composition, moisture, initial density, chamber geometry, feed mass, loading history, and post-compression recovery; rated compression force alone therefore cannot determine bale weight or density. Evidence role: mechanism; source type: paper. Supports: Compaction research should establish that final density is a multivariable outcome influenced by pressure together with material properties, moisture, geometry, feed mass, dwell or cycle conditions, and elastic recovery.. Scope note: The relative importance of each variable differs among cardboard, plastics, textiles, biomass, and metals. ↩